Medical & Surgical Products

Medical Product Packaging

Medical Product Packaging: 10 Important Benefits Every Buyer Should Know

Packaging plays an important role in the healthcare product supply chain. For medical consumables and healthcare products, packaging is not simply an outer covering. It can help with product identification, handling, storage, hygiene, traceability, and protection throughout transportation and use. Products such as medical gloves, cotton, gauze, dressings, tapes, orthopedic products, and medical devices may pass through several stages before reaching a healthcare professional. Appropriate packaging can help protect products during these stages and provide important information to healthcare buyers and users. However, packaging requirements vary depending on the product. Healthcare organizations should always follow the manufacturer’s labeling, instructions, and applicable requirements. What Is the Role of Packaging in Healthcare Products? Medical product packaging can serve several functions at the same time. It may help: Identify the product Protect the contents Provide product information Support safe handling Facilitate storage Protect against environmental exposure Maintain package integrity Support batch and lot identification Communicate expiry or shelf-life information Provide relevant usage or storage instructions The exact role depends on the product, its intended use, and the type of packaging used. 1. Packaging Helps Identify the Product Healthcare facilities may store hundreds or thousands of different medical products. Clear packaging helps staff distinguish between products that may look similar. Important information may include: Product name Product type Size Dimensions Quantity Material Product code Intended use Manufacturer information For example, different sizes of medical gloves may have similar packaging. Clear product identification can help staff select the correct size. Similarly, gauze products may differ in dimensions, layers, construction, or packaging format. Clear labeling helps healthcare buyers and staff distinguish between them. 2. Packaging Supports Product Handling Medical supplies can be transported and handled several times before they are used. Packaging can help make products easier to: Transport Carry Stack Store Count Distribute Identify Appropriate packaging can also help protect products from unnecessary physical handling. For larger healthcare facilities, products may move from: Manufacturer → Distributor → Central Medical Store → Department → Point of Use At each stage, packaging can help maintain product organization and identification. 3. Packaging Supports Storage Storage conditions can affect medical products, particularly when products are exposed to unsuitable environmental conditions. Packaging can provide a layer of protection against factors such as: Dust Moisture Light, where applicable Physical damage Contamination risks However, packaging should not be considered a substitute for proper storage conditions. Healthcare facilities should still follow the manufacturer’s specified storage requirements. Good Storage Practice Products should generally be: Stored in clean areas Protected from moisture Kept away from unnecessary contamination Protected from excessive heat where applicable Stored according to manufacturer instructions Kept in suitable original packaging where appropriate 4. Packaging Can Support Hygiene Hygiene is an important consideration for healthcare products. Packaging can help limit unnecessary exposure of products to the surrounding environment during transportation and storage. This can be particularly relevant for products that require controlled handling or specific packaging conditions. For products supplied as sterile, the packaging system is particularly important because package integrity is part of maintaining the product’s sterile state until use. Before Using a Packaged Medical Product Healthcare staff should check for: Tears Punctures Broken seals Open packaging Moisture damage Unusual contamination Missing or unclear labeling If packaging integrity is compromised, the product should be handled according to the healthcare facility’s established procedures. 5. Packaging Helps Protect Products During Transportation Medical products may travel long distances before reaching their final destination. During transportation, packages can potentially experience: Vibration Compression Impact Dust exposure Moisture exposure Temperature fluctuations Appropriate packaging can help reduce the risk of physical damage during handling and transportation. Outer cartons can also make it easier to organize products during bulk shipment. 6. Packaging Supports Product Traceability Traceability is important for healthcare products. Packaging may display information such as: Batch number Lot number Manufacturing information Product code Expiry date Manufacturer details This information can help healthcare organizations identify specific products within their inventory. Batch and lot information can also support inventory management and quality investigations where required. 7. Packaging Provides Expiry Information Many healthcare products have a defined shelf life or expiry date. Clear expiry information can help healthcare facilities manage inventory effectively. Staff can use expiry information to: Identify products approaching expiry Apply FEFO principles Reduce unnecessary wastage Prevent use of expired products Plan inventory rotation FEFO FEFO means First Expiry, First Out. Under this approach, products with the earliest expiry dates are generally prioritized for use or issue before products with later expiry dates, provided they remain suitable for use. 8. Packaging Communicates Storage Requirements Some healthcare products have specific storage requirements. The product packaging or accompanying documentation may communicate information relating to: Temperature Moisture Light exposure Handling Storage orientation Other product-specific requirements Healthcare facilities should review these instructions before storing products. Important There is no single storage condition that applies to every medical product. A product should be stored according to its manufacturer’s instructions and applicable requirements. 9. Packaging Helps Prevent Product Mix-Ups Healthcare facilities often manage products with similar names or appearances. For example: Different glove sizes Different gauze dimensions Sterile vs non-sterile products Different cotton formats Different tape sizes Different orthopedic products Clear packaging and labeling can reduce confusion during storage and distribution. Color coding or other visual identification may also be used by manufacturers, but staff should always confirm the actual product information rather than relying only on appearance. 10. Packaging Supports Inventory Management Good packaging can make inventory management easier by providing visible product information. Warehouse or medical-store staff can identify: Product Quantity Batch/lot Expiry Size Specification This makes stock counting and inventory recording more efficient. For large healthcare facilities, packaging information can also be captured in digital inventory systems. Packaging Requirements for Different Medical Products Different medical products may require different packaging approaches. Medical Gloves Packaging can help identify: Glove type Size Quantity Manufacturer Batch/lot Expiry information where applicable The packaging should protect gloves from unnecessary environmental exposure and physical damage. Cotton Products Packaging can help protect cotton products from: Dust Moisture Physical

Medical Product Packaging: 10 Important Benefits Every Buyer Should Know Read More »
Quality Checks

12 Must-Know Quality Checks for Safe and Reliable Medical Products

Healthcare facilities depend on medical products that are consistent, clearly specified, properly packaged, and manufactured under appropriate quality processes. Products such as medical gloves, cotton, gauze, surgical tapes, orthopedic supplies, dressings, and medical devices may be used regularly in hospitals, clinics, diagnostic centres, and other healthcare environments. For healthcare buyers, product quality is not determined by appearance or price alone. Consistent manufacturing processes, product inspection, accurate specifications, packaging checks, and appropriate manufacturing standards all contribute to a more reliable healthcare supply chain. Understanding these quality factors can help hospitals, clinics, distributors, and procurement teams make more informed purchasing decisions. What Does Quality Mean in Healthcare Products? Quality in healthcare products involves more than simply producing an item that looks acceptable. A quality-focused manufacturing process aims to achieve consistency in areas such as: Raw material selection Manufacturing processes Product dimensions Physical characteristics Packaging Labelling Batch consistency Storage requirements Applicable quality and regulatory requirements The specific quality requirements vary depending on the product and its intended use. Therefore, healthcare buyers should always review the manufacturer’s product specifications and applicable documentation. 1. Importance of Consistent Quality Processes Consistency is one of the most important aspects of medical product manufacturing. Healthcare facilities often purchase the same products repeatedly. If product characteristics vary significantly between batches, it can make procurement, inventory management, and product use more difficult. A consistent quality process can help manufacturers maintain predictable product characteristics from one production batch to another. Why Consistency Matters Consistent processes can help support: Uniform product characteristics Reliable manufacturing output Better inventory planning Easier product comparison Reduced variation between batches Greater confidence among healthcare buyers For example, when a healthcare facility repeatedly purchases a particular type of medical cotton, gloves, or gauze, consistent specifications can make routine procurement more predictable. 2. Importance of Product Inspection Inspection is an important part of quality management. Depending on the product, inspection may involve checking physical characteristics, dimensions, appearance, packaging, labelling, or other defined requirements. The exact inspection process should be based on the product’s specifications and applicable quality procedures. Inspection Can Help Identify Visible defects Incorrect dimensions Packaging problems Labelling issues Product inconsistencies Damage during handling or production Inspection does not replace a complete quality-management system, but it can be an important component of maintaining product consistency. 3. Why Clear Product Specifications Matter Product specifications provide measurable or defined information about what a product is supposed to be. For healthcare buyers, clear specifications make it easier to understand whether a product is suitable for its intended application. Specifications may include: Product name Material Size Dimensions Weight Quantity Product composition Intended application Packaging format Shelf life, where applicable Storage requirements Example A healthcare buyer purchasing cotton should know whether the requirement is for absorbent cotton, cotton rolls, dental cotton rolls, or another product format. Similarly, a buyer ordering medical gloves may need to consider material, size, intended application, packaging, and other product-specific characteristics. Clear specifications reduce ambiguity and help procurement teams compare products more effectively. 4. Packaging Checks Are an Important Quality Step Packaging is not simply an outer covering. It can help protect medical products during manufacturing, transportation, storage, and handling. Packaging checks can help identify problems such as: Torn packaging Punctures Broken seals Moisture damage Incorrect labels Damaged cartons Missing product information For products where packaging integrity is important, healthcare facilities should inspect packaging before placing products into use. If packaging appears compromised, the product should be handled according to the facility’s quality and safety procedures. 5. Manufacturing Standards and Quality Management Medical products should be manufactured under processes appropriate to their product category and intended application. Manufacturing standards and quality-management systems can provide a structured framework for areas such as: Production control Quality assurance Documentation Inspection Traceability Corrective actions Process monitoring Product release The specific standards or regulatory requirements applicable to a product depend on factors such as the product category, intended use, market, and applicable regulations. Healthcare buyers should therefore avoid assuming that one certification or standard applies equally to every medical product. 6. Raw Material Quality The quality of a finished healthcare product can be influenced by the materials used to manufacture it. Manufacturers may establish processes for selecting, receiving, evaluating, and controlling raw materials according to their quality systems and product requirements. For products such as medical cotton, gauze, gloves, tapes, and other consumables, appropriate raw material selection can contribute to consistent finished-product characteristics. Healthcare buyers can ask suppliers about relevant material specifications and quality documentation when appropriate. 7. Batch and Lot Traceability Traceability can be particularly useful in healthcare product supply chains. Batch or lot information can help manufacturers and buyers identify products associated with a particular production batch. Depending on the product, traceability information may support: Inventory management Quality investigations Product identification Expiry monitoring Complaint handling Product recalls, where necessary Healthcare facilities should maintain relevant batch or lot information according to their own procedures and applicable requirements. 8. Quality Checks Should Continue Beyond Manufacturing Quality does not end when a product leaves the production line. Products can potentially be affected by transportation, handling, storage, and distribution. A healthcare facility can therefore perform appropriate checks when receiving supplies. Receiving Inspection Checklist Before accepting products into inventory, buyers or receiving teams can check: Product: Is the correct product supplied? Quantity: Does the delivered quantity match the order? Packaging: Is the packaging intact? Labelling: Are product details and batch/lot information clear? Expiry: Is the product within its stated shelf life? Condition: Is there visible damage, contamination, or moisture exposure? Documentation: Is required product documentation available? These checks can help identify issues before products enter regular inventory. 9. Storage and Quality Go Together Even products manufactured under appropriate quality processes need suitable storage after delivery. Healthcare facilities should follow manufacturer storage instructions and protect products from conditions that could affect their quality or packaging. General considerations may include: Clean storage areas Moisture control Appropriate temperature according to manufacturer instructions Protection from direct sunlight where applicable Protection from physical damage Original packaging protection Proper stock organization Expiry

12 Must-Know Quality Checks for Safe and Reliable Medical Products Read More »

The Powerful Truth About Sterile Medical Supplies and Patient Safety

Sterile Medical Supplies play a vital role in protecting patients from infections and supporting safe medical care. Maintaining Patient Safety in Healthcare requires proper Medical Sterilization and the use of reliable Sterile Healthcare Products. High-quality Infection Prevention Supplies also help healthcare professionals reduce contamination risks and maintain hygienic treatment environments. Sterile medical supplies play an important role in maintaining patient safety in hospitals, clinics, and other healthcare facilities. Every day, healthcare professionals use medical products during wound care, surgical procedures, and routine patient treatment. However, medical supplies that come into contact with wounds or certain clinical areas may carry infection risks if proper sterility standards are not maintained. Therefore, using suitable sterile medical supplies is essential for safer patient care. Moreover, proper handling and storage of sterile products help healthcare facilities maintain hygiene and reduce unnecessary exposure to harmful microorganisms. What Are Sterile Medical Supplies? Sterile medical supplies are healthcare products that have undergone a controlled sterilization process to remove or destroy viable microorganisms. These products are commonly used in procedures where infection prevention is especially important. Common sterile medical supplies may include: • Sterile gauze swabs• Sterile wound dressings• Surgical gloves• Certain medical cotton products• Surgical drapes• Procedure-related disposable supplies Therefore, healthcare professionals should select suitable sterile products based on the clinical procedure and patient care requirements. Why Sterility Is Important for Patient Safety Patients may be exposed to microorganisms during medical procedures, wound treatment, or surgery. If contaminated medical products are used, the risk of healthcare-associated infections may increase. Sterile medical supplies help: • Reduce exposure to harmful microorganisms• Support safer wound care• Maintain hygiene during procedures• Protect vulnerable patients• Improve infection control practices As a result, sterility is an important part of modern healthcare safety. Role of Sterile Supplies in Infection Prevention Infection prevention is a major responsibility in every healthcare facility. Sterile products help create a safer environment during procedures that involve wounds, damaged skin, or other infection-sensitive areas. Additionally, proper sterile practices can support: • Better patient protection• Safer clinical procedures• Reduced contamination risks• Improved hospital hygiene• Effective infection control protocols Therefore, healthcare facilities should maintain proper standards when selecting and handling sterile medical supplies. Common Healthcare Areas That Require Sterile Supplies Sterile medical products are used across several healthcare departments. They are commonly required in: • Operation theatres• Emergency departments• Wound care units• Intensive care units• Maternity and delivery rooms• Outpatient procedure rooms• Diagnostic and treatment areas Moreover, the type of sterile supply required may vary depending on the procedure. Importance of Sterile Supplies in Wound Care Open wounds can be vulnerable to contamination and infection. Therefore, sterile wound care products are commonly used during wound cleaning, dressing, and protection. Sterile gauze and dressings can help: • Protect the wound area• Support clean dressing procedures• Absorb wound fluids when appropriate• Reduce unnecessary contamination• Support the healing environment Consequently, selecting suitable wound care products is important for effective patient management. Sterile and Non-Sterile Medical Supplies: Understanding the Difference Sterile and non-sterile medical products are designed for different healthcare applications. Sterile products are processed to meet defined sterility requirements and are commonly used for infection-sensitive procedures. In contrast, non-sterile products may be suitable for general healthcare activities where sterility is not required. Therefore, healthcare professionals should always select medical supplies according to their intended use and clinical requirements. How Improper Handling Can Affect Sterility Even a sterile medical product may become contaminated if it is handled incorrectly. For example, damaged packaging or poor storage conditions may affect product safety. Common handling mistakes include: • Opening sterile packaging too early• Touching sterile areas with unclean hands• Using products from damaged packaging• Storing supplies in unsuitable conditions• Using products beyond their expiry date Therefore, healthcare staff should carefully inspect medical supplies before use. Importance of Proper Storage of Sterile Medical Supplies Proper storage helps maintain the condition and integrity of sterile medical products. Sterile supplies should generally be stored in clean and suitable areas according to product and manufacturer requirements. Healthcare facilities should: • Keep supplies away from moisture• Maintain clean storage spaces• Protect packaging from damage• Organize products properly• Regularly check expiry dates Furthermore, effective inventory management can help prevent the use of unsuitable or expired products. Why Packaging Integrity Matters Packaging acts as an important protective barrier for sterile medical supplies. If packaging is torn, wet, punctured, or otherwise damaged, the sterility of the product may be compromised. Before using a sterile product, healthcare professionals should check: • Package condition• Seal integrity• Product expiry date• Visible signs of damage• Storage condition As a result, simple packaging checks can support better patient safety. Role of Healthcare Workers in Maintaining Sterility Healthcare professionals play an important role in maintaining sterile practices. Proper training and awareness can help reduce contamination during patient care. Healthcare workers should: • Follow hand hygiene practices• Use medical supplies correctly• Avoid unnecessary contact with sterile surfaces• Follow proper opening techniques• Dispose of used medical products safely Moreover, healthcare facilities should regularly reinforce infection prevention and sterile handling procedures. Benefits of Using Quality Sterile Medical Supplies Reliable sterile medical supplies support safer and more efficient healthcare practices. Their benefits include: • Improved infection prevention• Better patient safety• Safer wound management• Support for clinical hygiene• Reliable use during medical procedures Therefore, choosing quality medical products is an important part of healthcare management. Choosing Reliable Sterile Medical Products Healthcare facilities should carefully select medical supplies from reliable manufacturers and suppliers. Important factors may include: • Product quality• Suitable packaging• Clear product information• Manufacturing standards• Reliable supply availability Additionally, healthcare professionals should use each product according to its intended purpose and provided instructions. Trusted Medical and Healthcare Products by JMS Medicon Looking for reliable medical, surgical, and healthcare products? 📍 JMS Medicon Private LimitedPlot No-85, Padmalava Nagar, Trisulia,Cuttack, Odisha – 754005 📞 Phone: +91 9437040988📧 Email: jmsmedicon@gmail.com🌐 Website: jmsmedicon.com JMS Medicon supports healthcare facilities with quality medical and surgical products designed for reliable use in patient care. Supporting Patient Safety with Quality Medical Supplies Sterile medical supplies

The Powerful Truth About Sterile Medical Supplies and Patient Safety Read More »

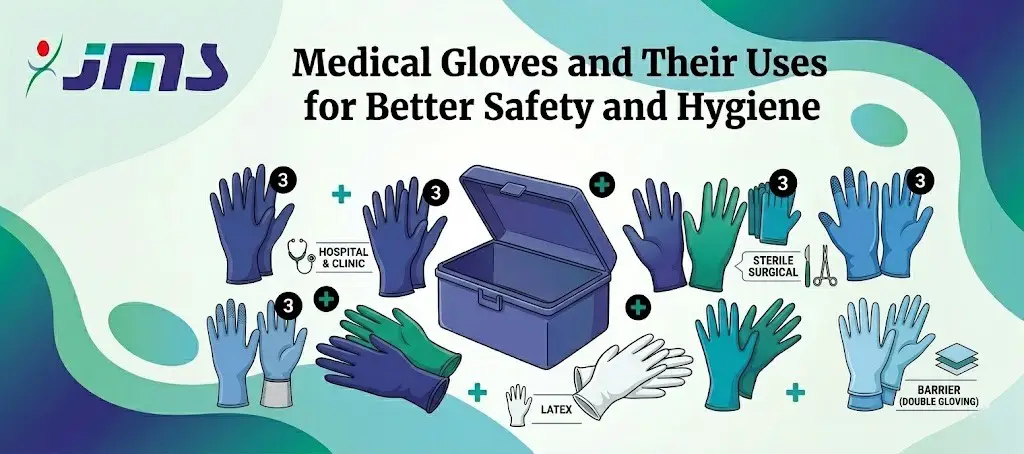
Informational infographic showing various medical gloves (blue, green, latex, sterile surgical, barrier) around a central medical kit to illustrate safety and hygiene uses.

Medical Gloves and Their Uses for Better Safety and Hygiene

Understanding different medical gloves types is important for maintaining hygiene, safety, and infection control in healthcare environments. Various gloves are designed for different medical purposes, including surgical gloves uses, routine examinations, and laboratory protection. High-quality sterile medical gloves help reduce contamination risks during procedures, while modern healthcare safety gloves improve protection for both patients and healthcare workers. In addition, understanding nitrile gloves benefits helps medical professionals choose durable and allergy-safe protective equipment. Different medical gloves types are used in hospitals and clinics depending on the procedure and safety requirements. Proper knowledge of surgical gloves uses, durable sterile medical gloves, and protective healthcare safety gloves helps maintain infection control standards. Many healthcare professionals also prefer nitrile products because of important nitrile gloves benefits such as flexibility, chemical resistance, and allergy protection. Choosing the correct medical gloves types improves safety, supports hygiene, and enhances medical protection during healthcare procedures.   Types of Medical Gloves and Their Uses Medical gloves are one of the most important protective products used in healthcare settings. They help maintain hygiene, reduce contamination, and protect both healthcare workers and patients during medical procedures. Today, different types of medical gloves are used for different purposes depending on the level of protection, comfort, and medical application required. Choosing the right glove is essential for ensuring safety and effective patient care. Why Medical Gloves Are Important in Healthcare Medical gloves create a protective barrier between the hands and potentially harmful substances. They help prevent: • Cross-contamination• Spread of infections• Exposure to blood and body fluids• Transmission of bacteria and viruses As healthcare standards continue to improve, the use of high-quality medical gloves has become even more important in hospitals, clinics, laboratories, and diagnostic centers. Latex Medical Gloves Latex gloves are among the most commonly used medical gloves because they offer excellent flexibility and comfort. These gloves are widely preferred for: • Surgical procedures• Medical examinations• Dental treatments• Laboratory work Advantages of latex gloves include: • High elasticity• Comfortable fit• Strong protection against contamination• Good touch sensitivity However, some people may develop latex allergies, which has increased the demand for alternative glove materials. Nitrile Medical Gloves Nitrile gloves are becoming increasingly popular because they are highly durable and latex-free. These gloves are commonly used in: • Hospitals• Emergency care units• Laboratories• Industrial medical settings Benefits of nitrile gloves include: • Strong puncture resistance• Excellent chemical resistance• Reduced allergy risk• High durability Additionally, nitrile gloves provide reliable protection in environments where exposure to chemicals or infectious materials is common. Vinyl Medical Gloves Vinyl gloves are generally used for short-duration and low-risk tasks. They are commonly suitable for: • Basic patient care• Cleaning tasks• Food handling• Non-invasive procedures Advantages include: • Cost-effectiveness• Latex-free material• Easy availability However, vinyl gloves may provide lower durability compared to latex and nitrile gloves. Surgical Gloves Surgical gloves are specially designed for operation theatres and sterile medical procedures. These gloves offer: • Precise fit• High sensitivity• Sterile protection• Better control during surgery They are manufactured under strict quality standards to ensure maximum safety during surgical procedures. Examination Gloves Examination gloves are used for routine medical examinations and patient care activities. Healthcare professionals commonly use them for: • Physical examinations• Diagnostic procedures• Blood sample collection• General patient interaction These gloves may be made from latex, nitrile, or vinyl depending on the requirement. Sterile vs Non-Sterile Gloves Medical gloves are also classified as sterile and non-sterile gloves. Sterile Gloves Sterile gloves are free from microorganisms and are mainly used for: • Surgical procedures• Invasive treatments• Sterile medical environments They help reduce the risk of infection during critical procedures. Non-Sterile Gloves Non-sterile gloves are commonly used for routine healthcare tasks such as: • Patient examinations• Cleaning procedures• Basic medical care These gloves still provide protection but are not intended for sterile surgical environments. Factors to Consider While Choosing Medical Gloves Selecting the right glove depends on the medical application and level of protection required. Important factors include: • Material type• Allergy concerns• Durability• Comfort and fit• Resistance to chemicals or punctures• Sterility requirements Healthcare providers should always choose gloves that meet proper safety and quality standards. Importance of Proper Glove Usage Even the best medical gloves are effective only when used correctly. Healthcare professionals should: • Change gloves between patients• Avoid reusing disposable gloves• Dispose of gloves safely• Wash hands before and after glove use Proper glove practices help maintain infection control and patient safety. Growing Demand for Disposable Medical Gloves The demand for disposable gloves has increased significantly in recent years due to greater awareness about hygiene and infection prevention. Medical gloves are now essential not only in healthcare but also in: • Pharmaceutical industries• Food industries• Laboratories• Home healthcare settings As healthcare systems continue to evolve, the importance of reliable protective equipment will continue to grow. Trusted Medical and Surgical Products by JMS Medicon Looking for reliable disposable medical gloves and surgical products? 📍 JMS Medicon Private LimitedPlot No-85, Padmalava Nagar, Trisulia,Cuttack, Odisha – 754005 📞 Phone: +91 9437040988📧 Email: jmsmedicon@gmail.com🌐 Website: jmsmedicon.com Medical gloves play a crucial role in maintaining hygiene, reducing infection risks, and protecting healthcare professionals during patient care. Choosing high-quality disposable gloves helps ensure safer healthcare environments and better protection for everyone involved.

Medical Gloves and Their Uses for Better Safety and Hygiene Read More »